

Standard calibration and testing operating procedures for AILEIKE pressure gauge
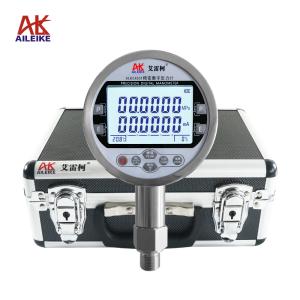
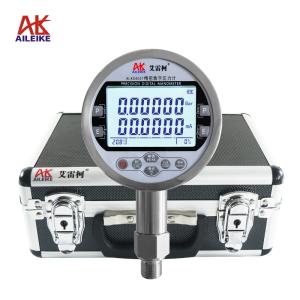
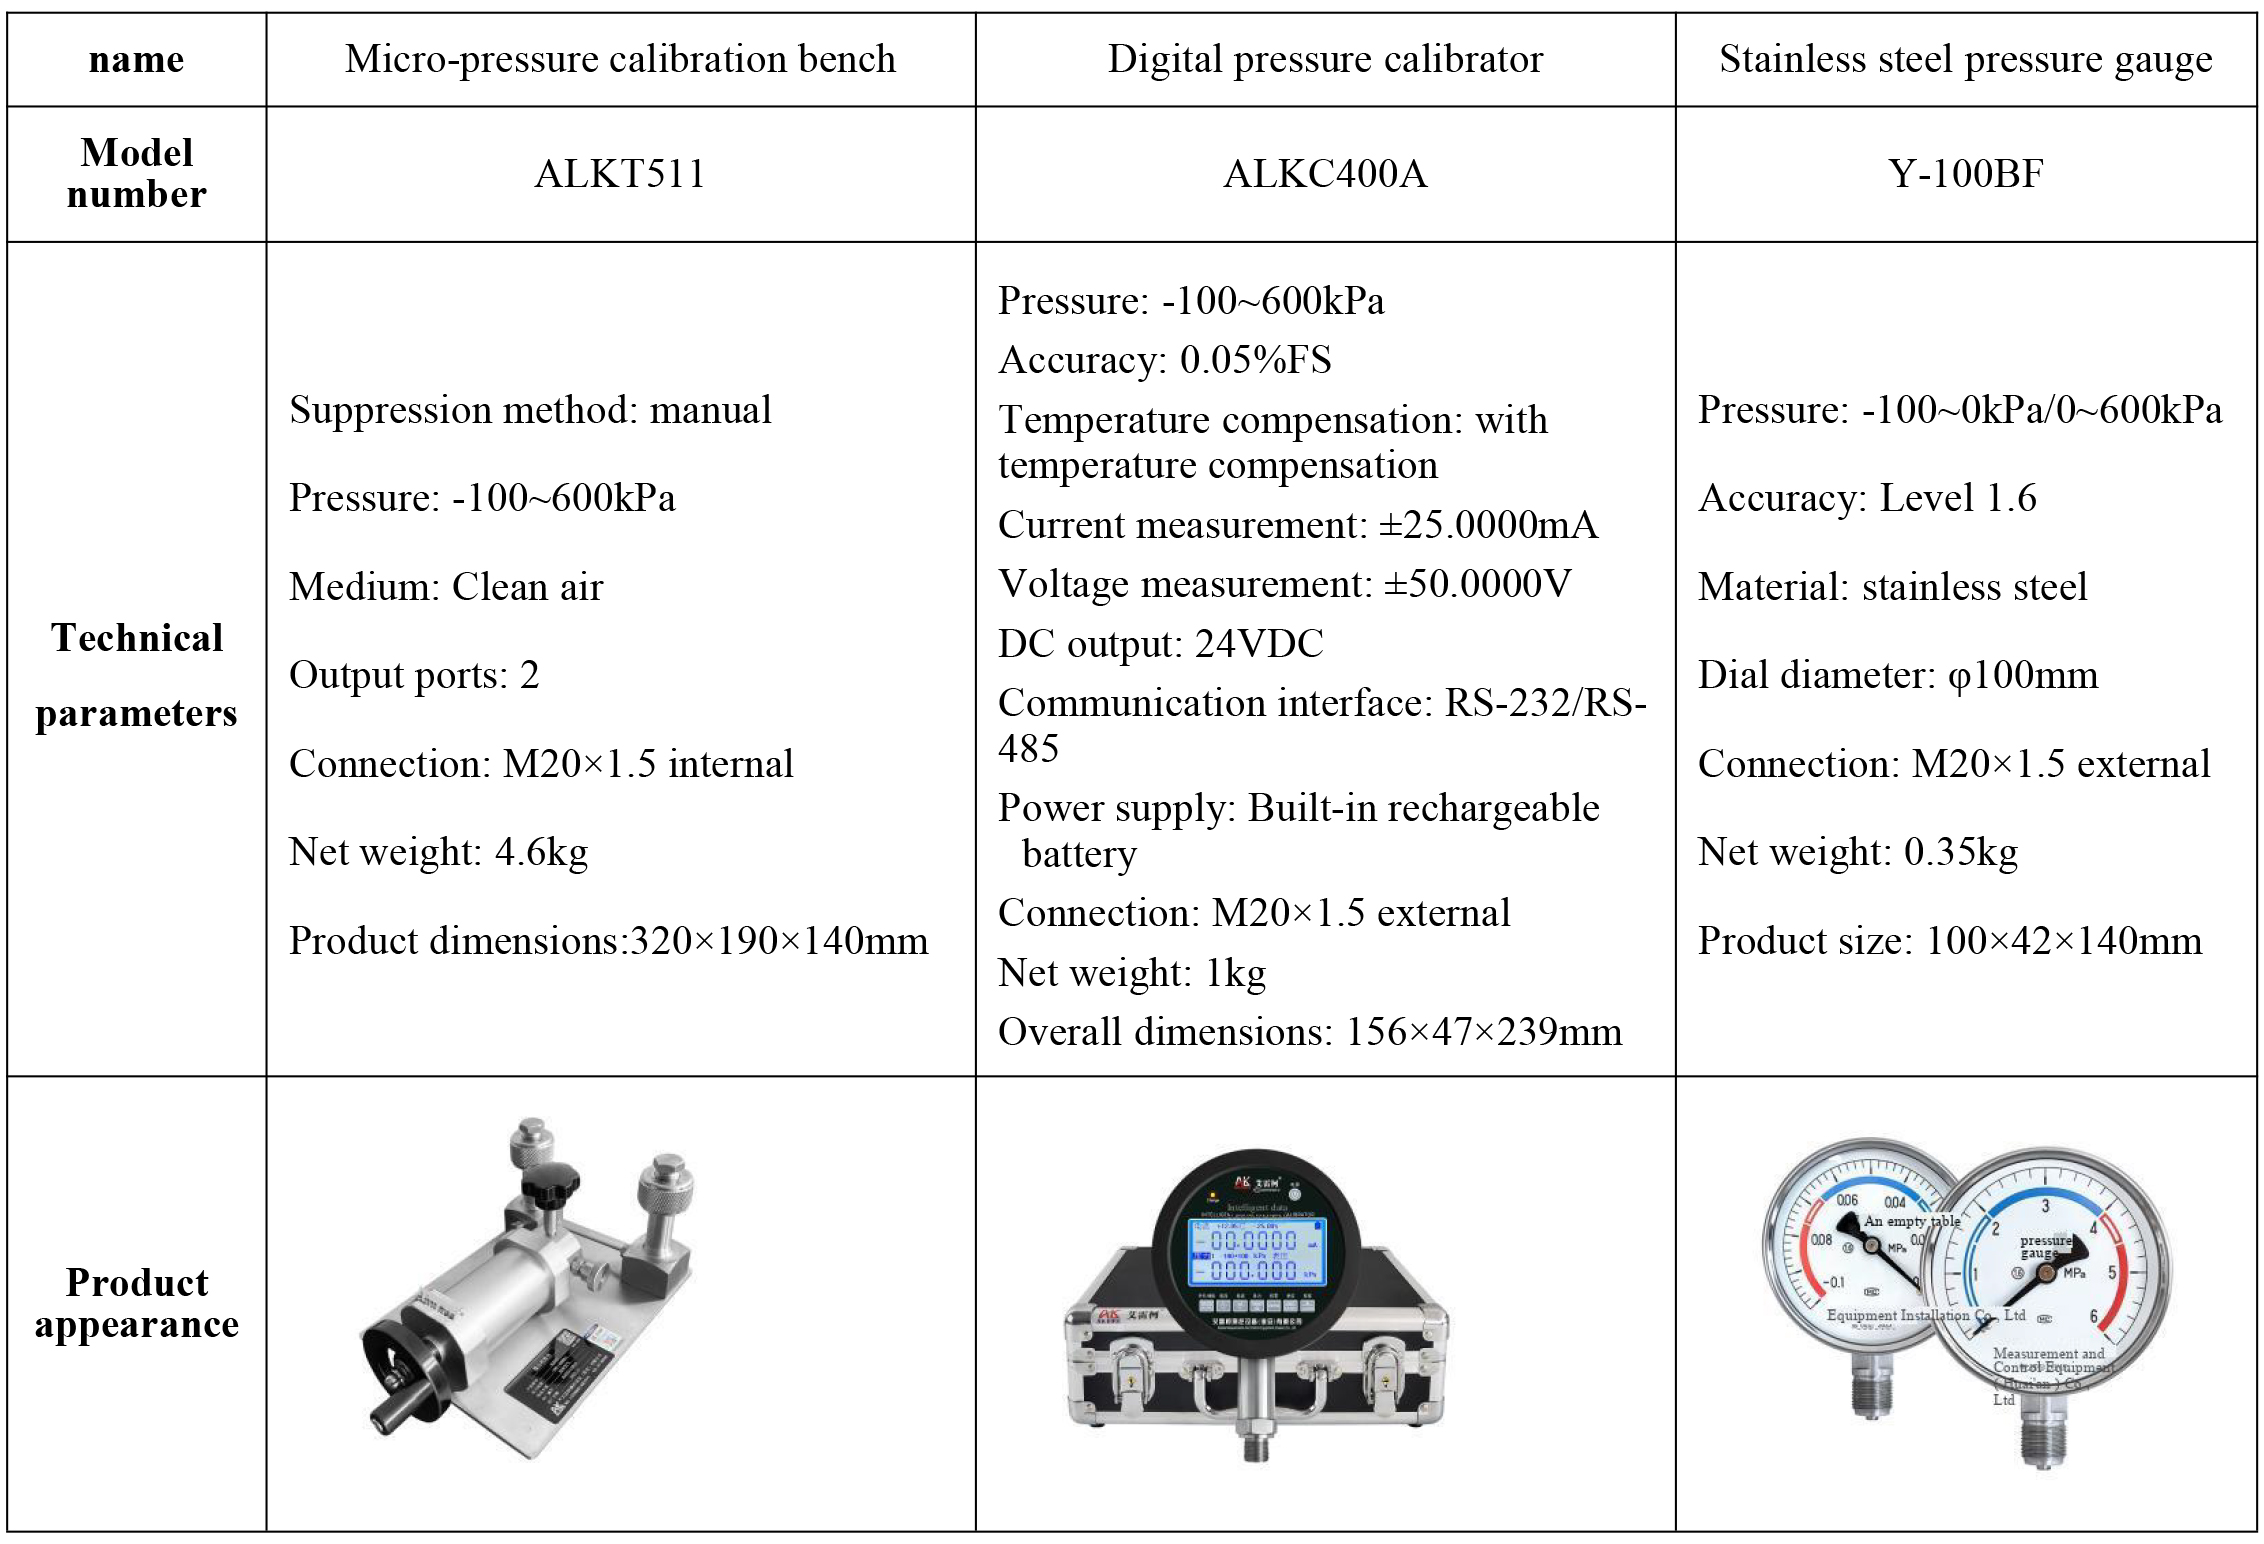
Pressure gauges are core pressure instruments used in industrial production and equipment calibration, and their measurement accuracy is crucial for data reliability. Therefore, it is particularly important to carry out standardized calibration, testing, and measurement work. This specification relies on the ALKT511 micro pressure calibration bench and the ALKC400A digital pressure calibrator to conduct fixed-point calibration and verification of stainless steel pressure gauges. The calibration strictly follows environmental standards of 20±2℃ and relative humidity ≤85% RH, completes instrument sealing and docking, and covers full-range testing of positive pressure and vacuum negative pressure. A step-by-step pressure increase and decrease operation is adopted. After stabilizing the pressure at a fixed point, the gauge case is tapped lightly, the indicated value is recorded, and the error is calculated. Throughout the process, metrological operation specifications are strictly adhered to, pressure is controlled smoothly to avoid shocks, and supporting instruments undergo annual verification. Standardized pressure relief and equipment maintenance mechanisms are established to ensure accurate and compliant pressure gauge measurements, providing reliable support for the quality standardization management of industrial equipment.
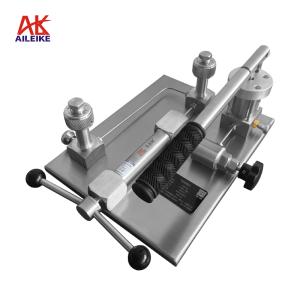
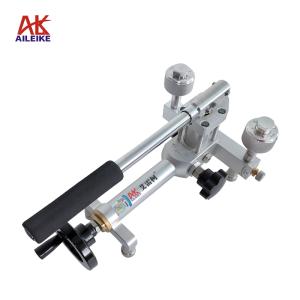
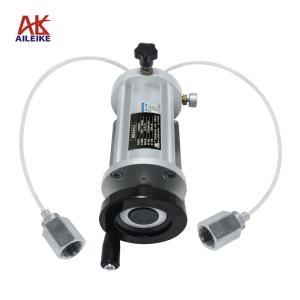
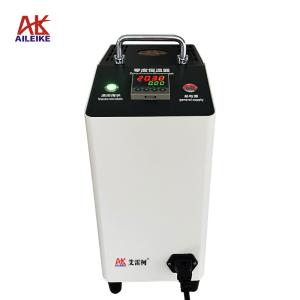
1. Calibration tool for pressure gauge
The entire verification process must strictly adhere to the current metrological technical specifications, primarily based on JJG52-2013 "Elastic Element Type General Pressure Gauges, Pressure Vacuum Gauges, and Vacuum Gauges". This standard is applicable to the initial verification, subsequent verification, and in-service inspection of elastic element type general pressure gauges, pressure vacuum gauges, and vacuum gauges, covering locally indicating pressure measuring instruments commonly used in industry.
II. Detailed Explanation of Operational Procedures
(I) Preliminary preparations
1. Environmental requirements
The temperature should be controlled at (20±2)℃, with a relative humidity of ≤85%RH, and there should be no condensation. Ensure that the site is free from vibration, dust, and corrosive gases.
2. Tool connection
Connect the standard gauge ALKC400A and the verified pressure gauge Y-100BF in a sealed manner to the ALKT511 output port.
(II) Pressure gauge calibration process
1. Voltage boosting process
First, open the pressure regulating valve of ALKT511, then turn the fine adjustment knob counterclockwise until it stops, and close the pressure relief valve.
• Rotate clockwise for pressure adjustment, increase the pressure to the verification value of 150kPa, and after the pressure stabilizes and the standard indicated value no longer fluctuates, check the pressure value of the verified pressure gauge. Then, gently tap the side of the verified pressure gauge's housing with your finger (tapping the glass or knocking hard is strictly prohibited), observe the pointer position, and record the indicated value after the tapping stabilizes. Use the indicated value after tapping as the actual measured verification reading for this pressure point, and calculate the error.
• For the same operation, use fine adjustment to rotate clockwise and apply pressure to the verification points of 300kPa, 450kPa, and 600kPa, check the pressure value of the verified pressure gauge, tap the verified pressure gauge, and record the indicated value after the tap becomes stable.
2. Decompression process
• First, slowly open the pressure relief valve and reduce the pressure to around the verification value. Close the pressure relief valve, and then use fine adjustment to gradually adjust it to the verification point of 450kPa. Once the pressure stabilizes, tap the verified pressure gauge and record the value.
• Perform the same operation with the verification points adjusted to 300kPa and 150kPa, check the pressure value of the verified pressure gauge, tap the verified pressure gauge, and record the indicated value after the tap stabilizes.
3. Pressure relief process
Open the pressure relief valve, gradually release the pressure inside the pipeline, and when the pressure relief reaches 0, the measurement is complete.
(III) Pressure gauge vacuum calibration process
1. Voltage boosting process
First, remove the verified meter for measuring positive pressure, install the verified meter for measuring negative pressure, turn the fine adjustment clockwise until it stops, and then close the pressure relief valve.
• Rotate counterclockwise for fine adjustment and apply pressure until reaching the verification value of -25kPa. Once the pressure stabilizes, tap the verified pressure gauge and record the value.
• Perform the same operation with the verification points set to -50kPa, -75kPa, and -100kPa, observe the pressure values of the verified pressure gauge, tap the verified pressure gauge, and record the indicated value after the tap stabilizes.
Note:
• When fine-tuning the vacuuming process and the fine adjustment fails to work, and the verification value is not reached, secondary pressurization is required.
• Secondary pressurization steps: First, close the pressure regulating valve, then open the pressure relief valve, and adjust the fine adjustment knob clockwise until it cannot be turned any further. Close the pressure relief valve, then open the pressure regulating valve, and use the fine adjustment knob to adjust counterclockwise to the verification point.
2. Decompression process
• First, slowly open the pressure relief valve to reduce the pressure to around the verification value, then close the pressure relief valve, and use fine adjustment to gradually adjust it to the verification point of -75kPa. Once the pressure stabilizes, tap the verified pressure gauge and record the value.
• Perform the same operation with the verification points adjusted to -50kPa and -25kPa, check the pressure values of the verified pressure gauge, tap the verified pressure gauge, and record the indicated value after it stabilizes.
3. Pressure relief process
Open the pressure relief valve, gradually release the pressure inside the pipeline, and when the pressure relief reaches 0, the measurement is complete.
III. Precautions
Standardized usage
• During verification, it is important to ensure that the tolerance of the standard instrument is less than that of the instrument being verified, to ensure the accuracy and reliability of the verification results and comply with metrological specifications.
• Operations should follow standard procedures. The ALKT511 micro-pressure calibration bench should be pressurized and depressurized slowly to avoid pressure shock.
• Increase the pressure to the verification point and record the indicated value after the standard gauge value stabilizes. For the verified pressure gauge, tap the gauge case after the pressure stabilizes, and take the indicated value after tapping as the accurate reading to ensure accurate recording.
• After the inspection is completed, slowly release the pressure to zero and ensure there is no residual pressure before removing the inspected instrument.
Maintenance and calibration cycle
• Regularly conduct metrological verification on the digital pressure calibrator ALKC400A (it is recommended to do so once a year) to ensure that the measurement accuracy meets the required standards.
• When the pressure gauge is not in use, the power should be turned off. If it is not used for a long time, it should be charged once every three months.
• If the micro-pressure stage is not in use for a long period, it should be depressurized before storage and covered with a cloth cover to prevent dust from entering the instrument.
IV. Conclusion
The full-range calibration and testing of pressure gauges rely on AILEIKE calibration equipment, strictly following standardized metrological procedures to complete the measurement, verification, and data calculation of positive and negative pressure ranges. The operation strictly controls environmental conditions such as temperature, humidity, and cleanliness, standardizes instrument sealing and docking, step-by-step pressure increase and decrease, stable pressure readings, light tapping for gauge calibration, and error calculation, avoiding pressure shocks and ensuring the authenticity and accuracy of data at each verification point. At the same time, it clarifies equipment operation specifications, annual periodic verification, and daily maintenance requirements, and implements this process on a regular basis to ensure that pressure gauge measurement and metrology are compliant and reliable, laying a solid metrological foundation for industrial equipment operation and maintenance and quality control.
Related News